Autonomous Mobile Robots for Smarter Material Flow
Discover KUKA's wide range of mobile robotics that cover the entire value creation chain, perfectly meeting the requirements of intralogistics and production in the new networked industry.
Mobilize Your Production
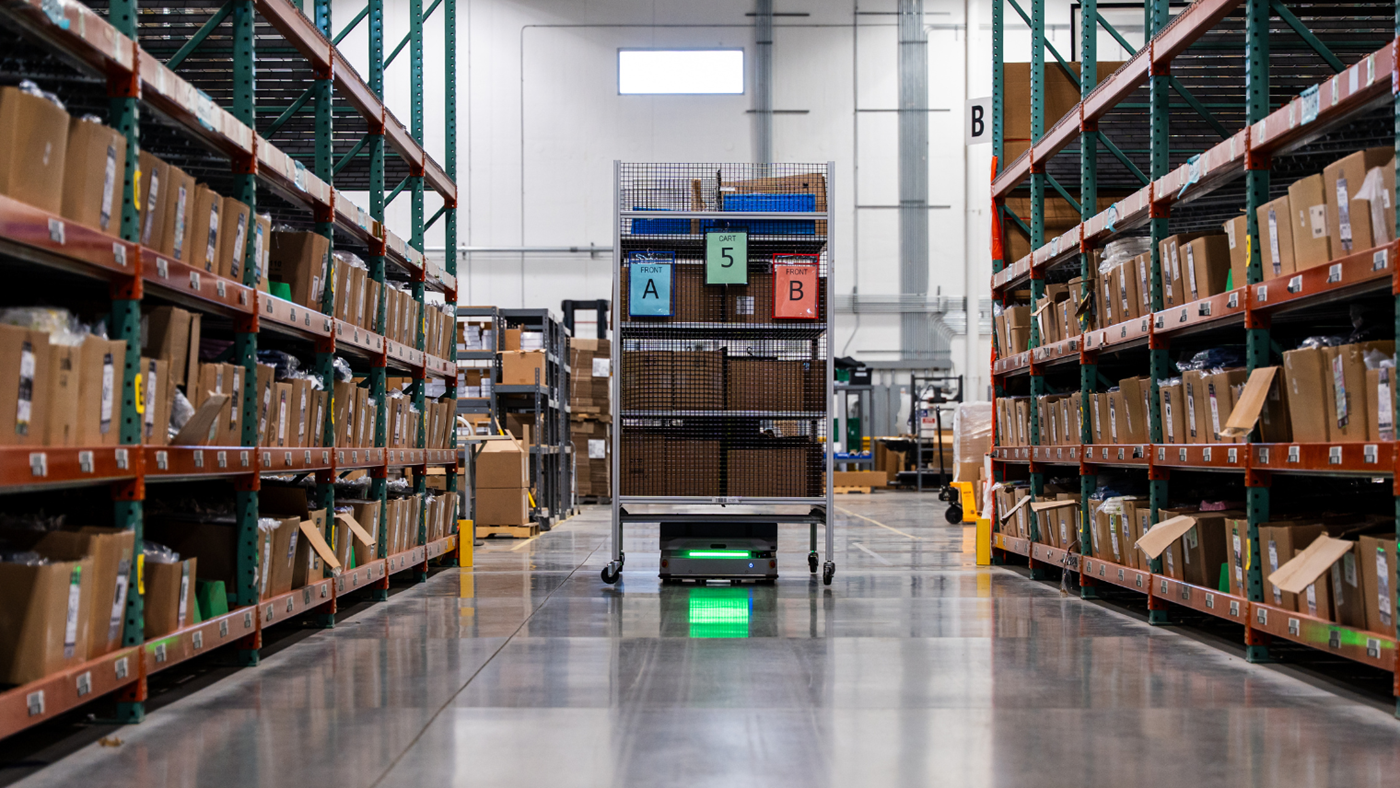
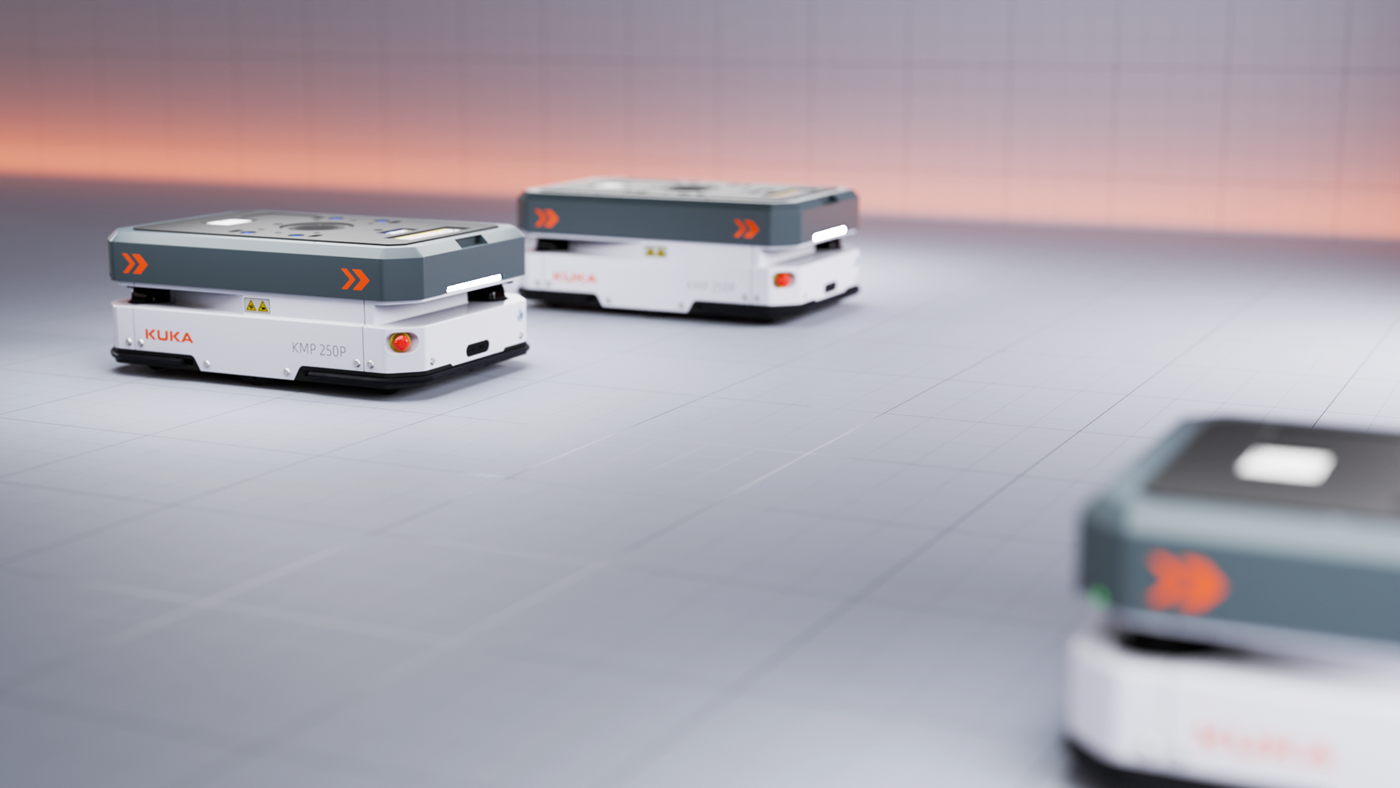
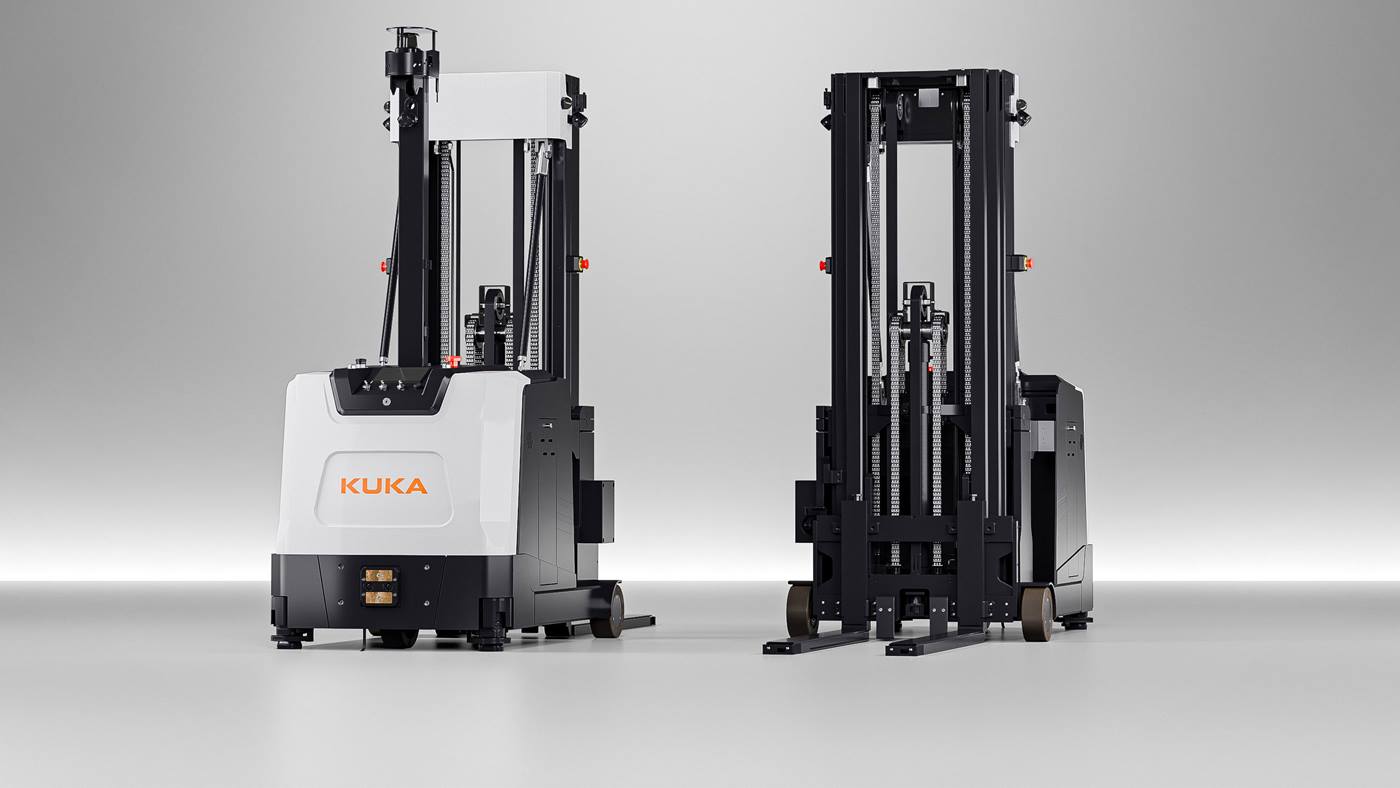
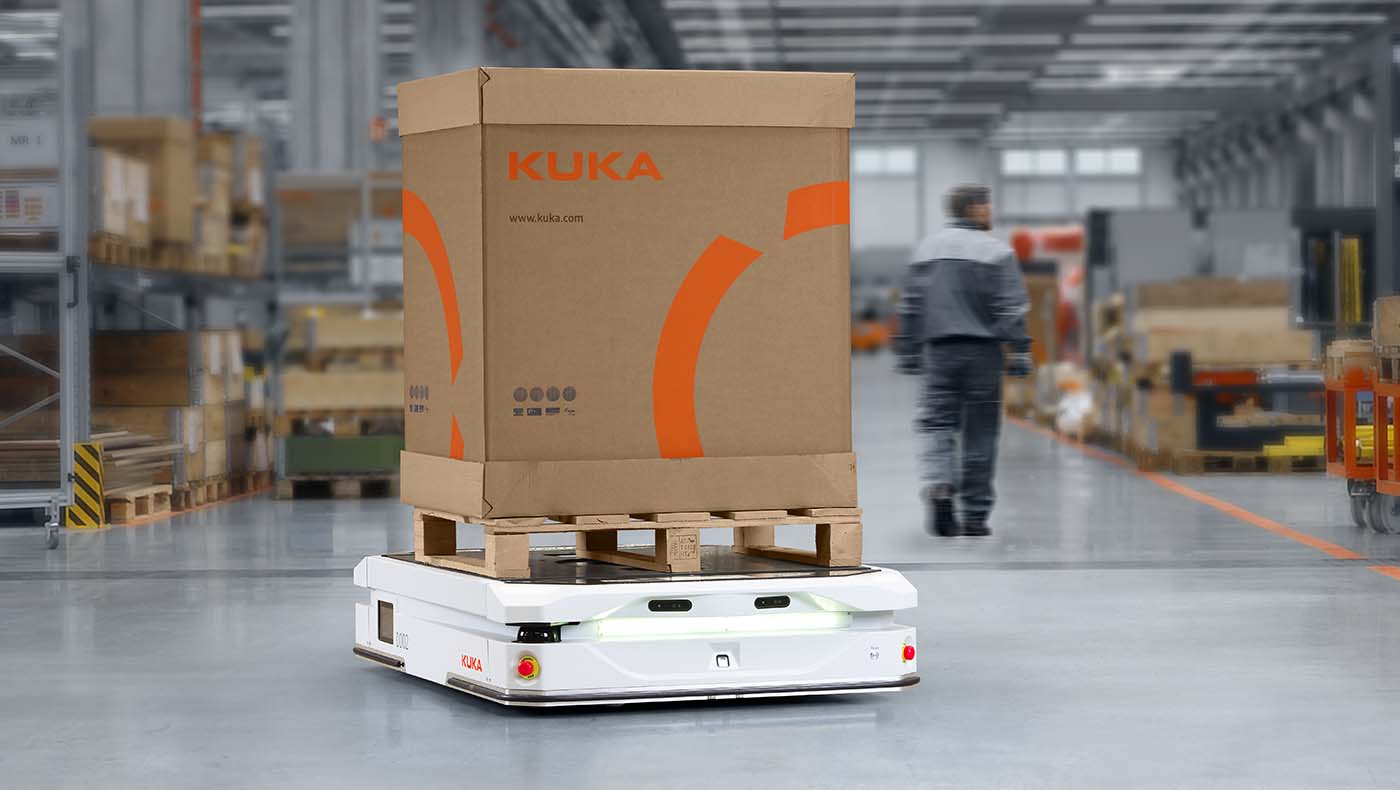
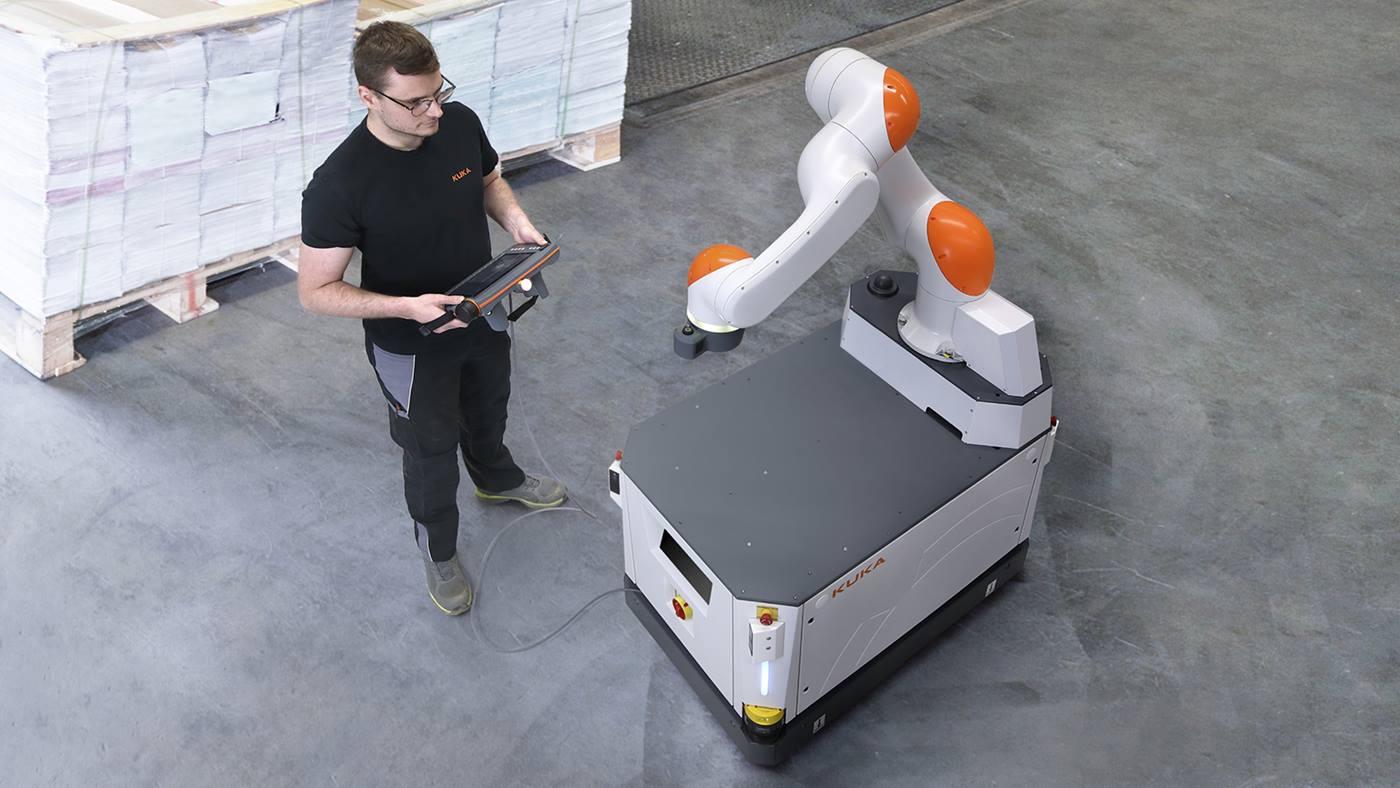
Keep materials, parts, and products moving with flexible autonomous mobile robots (AMRs) from KUKA. From compact material transport to heavy-load handling, pallet movement, and autonomous forklifts, KUKA provides scalable mobile robotics solutions for manufacturing, warehousing, and intralogistics.
Automate material flow without relying on fixed conveyors or traditional guided systems. KUKA AMRs navigate dynamically, adapt to changing production environments, and integrate with your broader automation ecosystem.

A Smarter Approach to Material Handling
Material flow can have a major impact on production efficiency. Manual transport, forklift traffic, labor availability, and fixed conveyor systems can create bottlenecks that limit productivity and flexibility.
KUKA AMRs help automate repetitive material movement while giving manufacturers and warehouse operators the flexibility to adapt as production needs change. Advanced sensors, intelligent navigation, and fleet management technology allow AMRs to safely navigate dynamic environments, avoid obstacles, and keep materials moving where they are needed.
KUKA AMRs help automate repetitive material movement while giving manufacturers and warehouse operators the flexibility to adapt as production needs change. Advanced sensors, intelligent navigation, and fleet management technology allow AMRs to safely navigate dynamic environments, avoid obstacles, and keep materials moving where they are needed.
Benefits of Autonomous Mobile Automation
- Increase productivity: Automate repetitive transport tasks and keep production supplied.
- Improve flexibility: Adapt routes and workflows as layouts and production requirements change.
- Address labor challenges: Shift repetitive material transport away from employees and forklifts.
- Scale automation: Start with individual vehicles and expand into coordinated AMR fleets.
- Optimize floor space: Reduce dependence on fixed conveyor infrastructure.
- Connect operations: Integrate mobile robotics with production equipment and ERP, MES, and WMS systems.